How to Choose a Comprehensive Checking Fixture?
A Comprehensive Checking Fixture can protect a production line from costly fit, alignment, and assembly errors. But a fixture is only useful when it reflects the part’s real datums, tolerances, and inspection sequence. A polished design can still fail. The mismatch may be as small as a poorly placed locating pin or a clamp that distorts a thin panel.
Industry guidance offers a practical starting point. AIAG’s Measurement Systems Analysis reference manual explains how repeatability and reproducibility affect confidence in inspection results. NIST dimensional metrology publications likewise emphasize traceable measurement and uncertainty. These references do not prescribe one universal fixture design; part geometry, inspection frequency, and process variation still matter. H. James Harrington, a quality-management expert, put the measurement principle plainly: “Measurement is the first step that leads to control and eventually to improvement.” That idea applies directly to fixture selection, but it does not replace validation on the actual part.
Look closely at the details. Can an operator load the component without forcing it? Do the locators contact stable surfaces? Can probes reach critical features, and can the fixture be checked against a master or calibrated reference? Consider material, wear, cleaning, storage, and future model changes, too. A fixture that saves seconds today may create rework later. There is no perfect checklist; even experienced teams can miss a changing process condition. The right Comprehensive Checking Fixture is the one that delivers repeatable, traceable results under real production conditions—and can be reviewed when those conditions change.
Define the Inspection Requirements and Part Characteristics
A comprehensive checking fixture starts with a clear definition of what must be inspected and why.
Identify critical dimensions, datum surfaces, hole locations, profiles, and assembly interfaces. Separate features that affect fit or function from those used only for process monitoring. A mounting hole, for example, may need a position check relative to two datums, not just a diameter check. Be precise.
Then study the part itself.
Thin stamped panels can flex under clamping, while cast parts may vary around rough surfaces. Note the material, wall thickness, expected variation, and any areas that are difficult to reach with a probe or gauge. Small shifts matter. Also consider the part’s natural resting position and how an operator will load it. A fixture that forces a flexible component flat may report a result that the finished assembly never experiences.
Define how results will be judged before choosing locating pins, supports, and clamps.
Specify tolerances, measurement points, inspection frequency, and whether the fixture needs to distinguish small dimensional changes. Record the method so different operators can repeat it. In practice, requirements are sometimes incomplete; that uncertainty should be discussed and resolved, rather than hidden behind a complicated fixture. Test the setup with real parts, including pieces near tolerance limits, and review whether the readings are stable and practical on the production floor.
Identify Datums, Tolerances, and Measurement Methods
A comprehensive checking fixture starts with clear datum choices. Identify the surfaces or holes that locate the part during assembly, then reproduce those references in the fixture. For a stamped panel, this might mean resting it on three defined pads and locating it with two pins. Avoid relying on a flexible edge that shifts under light pressure. Small errors matter.
Set tolerances from the part drawing and its functional requirements, not from fixture convenience. A tight tolerance may need a stable locating scheme and careful temperature control; a noncritical feature may not. Record the allowed variation for each checked dimension, along with the fixture’s own repeatability. If the first setup produces inconsistent readings, revisit the datums before tightening the inspection process.
Choose measurement methods that suit the feature and production pace. Pins can check hole position, while a dial indicator can reveal surface variation across a panel. A coordinate measuring machine may help verify complex geometry, but it is not always practical for every part on the line. Compare fixture readings against an independent measurement during validation. The best method can still miss a problem if the part is loaded differently each time, so document hand placement and clamping force. Some choices will need adjustment after real parts arrive. That is worth admitting early.
How to read this example: The bars show illustrative drawing tolerances, not universal limits. Establish primary, secondary, and tertiary datums from the part design, then choose a measurement method suited to each feature. Confirm all tolerance values and inspection requirements against the actual drawing.
Evaluate Fixture Design, Accessibility, and Repeatability
How to Choose a Comprehensive Checking Fixture?
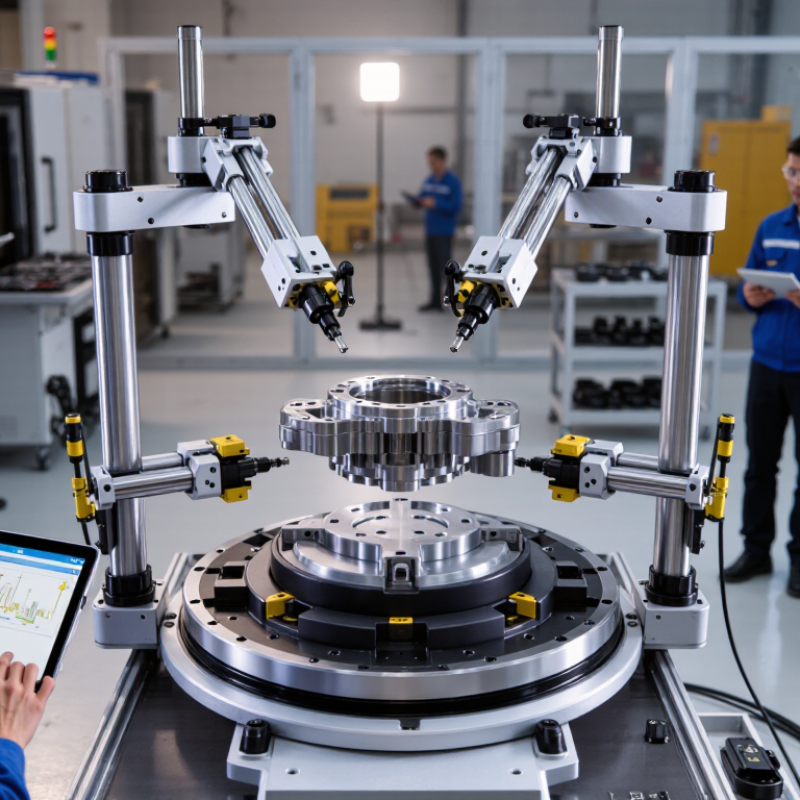
Evaluate fixture design, accessibility, and repeatability before approving a checking fixture. Its locating points should match the part’s functional datums, not merely convenient edges. Check that clamps hold the part securely without bending thin walls or changing its shape. A stop that looks solid may still shift under pressure. Small details matter.
Accessibility affects both speed and measurement quality. Operators should be able to load the part in one clear orientation and reach probes, gauges, and inspection points without awkward hand positions. Leave enough clearance for the measuring tool, while keeping the part supported near critical features. If a probe must enter at an angle, confirm that the approach is practical on the shop floor. I have seen simple access issues create inconsistent readings.
Tips: Run repeated checks after removing and reloading the part. Ask different operators to use the fixture, then compare results across several representative parts. Watch for variation caused by debris, clamp force, or locator wear. Record any setup steps that feel unclear; those are worth revisiting, even if the first trial passes.
Select Materials, Components, and Calibration Features
How to Choose a Comprehensive Checking Fixture?
Select Materials, Components, and Calibration Features
Choose fixture materials around the part, production volume, and inspection environment. Aluminum keeps a large fixture lighter and easier to reposition. Steel resists wear at frequently used locating points. Polymer contact pads can protect delicate surfaces, but they may compress over time. Fit matters. Check how temperature changes affect both the part and fixture, especially when measurements are tight.
Specify repeatable locators, stable supports, and clamps that hold parts without distorting them. Add probe access, clear datum references, and replaceable wear components where practical. Deloitte and MAPI’s 2019 Smart Factory Study found that 86% of surveyed manufacturers expected smart factories to drive competitiveness within five years. That finding supports designing fixtures for connected inspection, but sensors cannot fix poor datum control.
Build calibration into the fixture’s design. Include accessible reference points or dedicated features for checking locator position and probe alignment. NIST Technical Note 1297 describes expanded measurement uncertainty using a coverage factor of k = 2, typically associated with roughly 95% coverage under stated assumptions. Record calibration results, environmental conditions, and adjustment history. Keep the records simple enough to maintain. A fixture can be beautifully engineered and still drift; that part deserves honest attention.
Validate the Fixture and Assess Supplier Support
Before approving a checking fixture, test it with representative parts, not only a polished sample. Include parts near the expected tolerance limits. Load each one using the documented sequence, then check whether locating pins seat fully and clamps close without forcing the part. Small details matter. A faint gap at a datum can change a measurement.
Repeat the setup several times, ideally with different operators. Compare readings against an agreed reference method, such as a calibrated gauge or coordinate measuring machine. Record the results, setup conditions, and any adjustments. If readings vary, investigate before accepting the fixture; operator technique may be part of the problem. It is not always obvious. Ask the supplier for clear inspection records, maintenance guidance, and training for your team. Confirm how quickly they can answer questions, replace worn components, and support design changes. A short response time is useful, but practical documentation matters more when production is waiting. Check that drawings and fixture markings match the current revision. Some checks may still feel awkward, and that deserves another review.