65337ed57a

Leave Your Message

Who Are the Top Part Fixture Manufacturers in China?

Choosing a Part Fixture manufacturer in China takes more than comparing prices or browsing polished product photos. A fixture may look simple, yet small errors in locating pins, clamp pressure, or datum surfaces can affect an entire production run. Details matter. Buyers should examine a supplier’s machining capability, inspection process, material records, and experience with similar parts. Ask how the team checks repeatability, handles design changes, and documents critical dimensions. A clear answer is useful; a vague promise is not.

This guide explores manufacturers that serve different production needs, from custom workholding solutions to repeat orders for established lines. It also considers practical factors such as sample approval, engineering communication, lead time, and after-sales support. These details can reveal how a supplier works when drawings change or a tolerance proves difficult to hold. No supplier is perfect. That is worth admitting. A company with advanced equipment may still be a poor fit if communication is slow or inspection records are incomplete. Likewise, a smaller workshop may offer attentive engineering support but lack capacity for large orders. Use the comparisons as a starting point, then verify claims through technical discussions, sample parts, and current references. The right choice depends on your part geometry, process, quality expectations, and production schedule—not on a ranking alone.
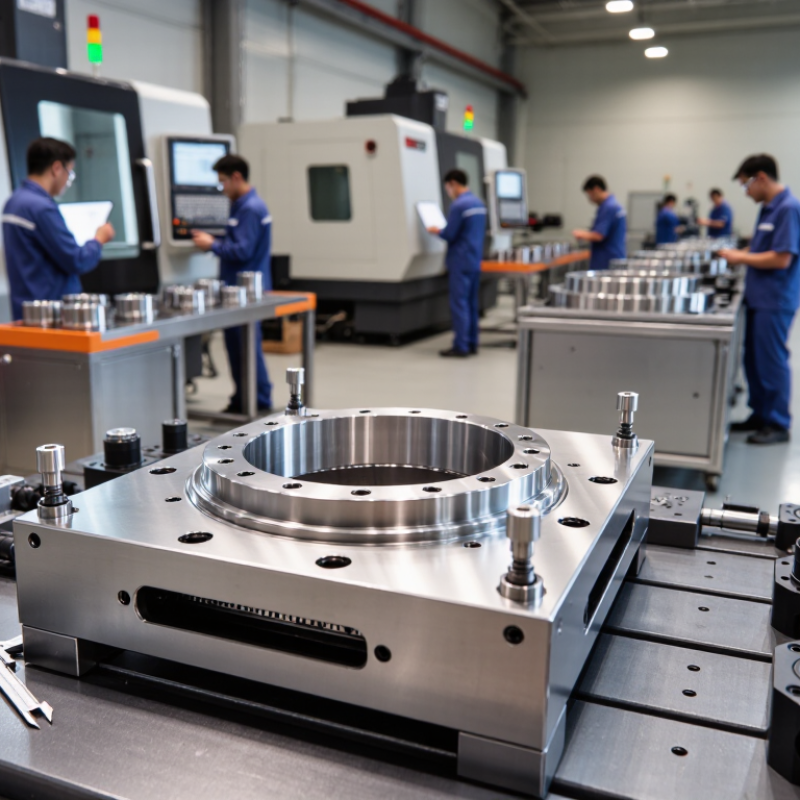
Who Are the Top Part Fixture Manufacturers in China?

Part Fixtures Explained: 3-2-1 Locating Constrains Six Degrees of Freedom

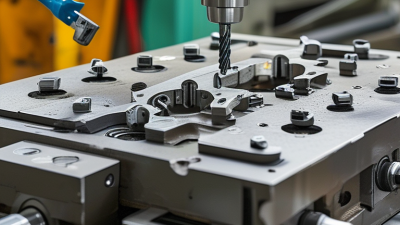
A part fixture works only when its locating scheme is deliberate. With 3-2-1 locating, three contacts support the primary plane, two locate a secondary plane, and one fixes the final direction. Together, they constrain six degrees of freedom: three translations and three rotations. Picture a machined block resting on three hardened buttons, touching two side stops, then one end stop. Clamps hold it down; they should not become extra locators.

That distinction matters. Extra or poorly placed contacts can rock a part, distort thin walls, or make repeatability depend on operator pressure. In the 2020 Deloitte and MAPI Smart Factory Study, 86% of 600 executives identified smart manufacturing as a future competitiveness driver. That survey measures executive expectations, not fixture accuracy. Fixture acceptance still needs evidence: repeatable seating, clearance checks, and measurements across real loading cycles. Real parts vary. A carefully designed CAD contact pattern may still fail against burrs, weld spatter, or a worn locator.
How Chinese Fixture Makers Engineer Accuracy, Clamping, and CNC Compatibility

Chinese part-fixture makers compete on more than low-cost machining. Accuracy starts with the datum scheme: a locating pin, a machined support, and a clean contact face must hold the workpiece in a repeatable position. Good designs also control clamp force. Too much force can distort a thin aluminum part; too little allows movement during cutting. Small details matter, including chip-clearance grooves and tool access around each clamp.

CNC compatibility means checking the fixture against the machine’s table, tool path, probe routine, and changeover needs. Fortune Business Insights estimated the global CNC machine market at US$83.99 billion in 2023 in its CNC Machine Market report. That figure signals broad investment in CNC capacity, but it does not prove any fixture’s accuracy. Ask suppliers for inspection records, repeatability results, and a trial cut on representative parts. A drawing alone is not enough.

Tip: Test with the actual workpiece. Record clamp torque, probe offsets, and part variation across repeated setups. Then review the results with the machinist. One weakness remains easy to miss: a fixture may pass inspection yet become awkward when chips collect beneath a support. Look again after a real production run.

How Fixture Makers Engineer Clamping for CNC Machining

Calculated theoretical hydraulic clamp force at 7 MPa for different cylinder bores.

Force is calculated as pressure × piston area. Actual clamping force can be lower because of friction, pressure losses, and linkage geometry. Fixture accuracy and CNC compatibility also depend on locating features, machine-table interfaces, and tool-clearance requirements.

Quality Benchmarks: ISO 2768-1:1989, CMM Inspection, and Repeatability

For a part fixture, ISO 2768-1:1989 can provide general tolerances for specified linear and angular dimensions that lack individual tolerances. The drawing should identify the tolerance class and show which dimensions it covers. A dowel-hole position or clamp-pad height may need its own tighter limit if fixture function depends on it. The standard is a baseline, not a substitute for design judgment.

CMM inspection helps verify critical features against the drawing’s datums. For example, an inspector can measure the distance between a mounting face and a locating pin, then compare the result with the stated tolerance. Probe strategy and datum alignment matter; a neat report can still reflect a poor setup. Keep the part clean, secure, and at a stable temperature before measurement. Small details count.

Repeatability means getting consistent results when the same feature is measured again under controlled conditions. Check several parts and repeat measurements after removing and repositioning a sample. If readings shift, review clamping force, probing direction, and operator method before changing the machining process. There is no universal repeatability target for every fixture. Set acceptance limits around the assembly’s actual locating and clamping needs, and retain inspection records. Even a careful process can miss variation between shifts, so periodic checks are worth the time.

Who Are the Top Part Fixture Manufacturers in China? - Quality Benchmarks: ISO 2768-1:1989, CMM Inspection, and Repeatability

Use this supplier-evaluation framework to compare part-fixture manufacturers. It lists verifiable quality benchmarks rather than company-specific rankings or performance claims.

Evaluation dimension What the benchmark means Evidence to request How to compare suppliers
General dimensional tolerances ISO 2768-1:1989 specifies general tolerances for linear and angular dimensions when an individual tolerance is not indicated. Its tolerance classes are fine (f), medium (m), coarse (c), and very coarse (v). A drawing showing the specified class, plus an inspection report for dimensions relevant to the fixture. Check that the drawing states the applicable class and that tighter functional requirements are individually toleranced. Do not treat a general-tolerance class as proof that every feature meets a particular tolerance.
Geometric and functional requirements Fixture performance can depend on datum locations, locating features, clamping interfaces, and geometric tolerances that are defined on the part or fixture drawing. A ballooned drawing or inspection plan linking each critical requirement to a measurement method and result. Compare whether critical locating and mating features are explicitly identified and inspected, rather than relying only on overall dimensions.
CMM inspection capability A coordinate measuring machine (CMM) can measure three-dimensional feature locations and geometry. The ISO 10360 series covers acceptance and reverification testing for CMMs; CMM use by itself does not guarantee a correct result. A sample CMM report, the measured feature list, equipment identification, and applicable calibration or reverification records. Confirm that the measurement setup and report address the drawing’s critical features. Ask how measurement uncertainty and probe access are considered.
Repeatability Repeatability describes the variation in results under defined, consistent measurement conditions. It is not a universal pass value; the acceptance limit should be agreed for the application. Repeated measurements of selected critical features, with the number of runs, setup, measurement method, and results recorded. Compare the observed spread or other agreed statistical measure against the project’s specified limit, using the same measurement conditions.
Measurement traceability Traceability connects measurement results to recognized measurement standards through a documented calibration chain. Current calibration records for relevant measuring equipment and identification linking the equipment to inspection results. Check equipment status and records for the instruments used on the specific fixture inspection; do not infer traceability from equipment brand or type alone.
Material and build documentation Fixture materials and components should be selected for the intended service conditions, such as load, wear, corrosion exposure, and required maintenance. A bill of materials, material certificates where specified, and records for purchased components relevant to the design. Verify that supplied materials and components match the drawing and purchase specification, and that substitutions are documented and approved.
Inspection and revision control Inspection results need to correspond to the correct drawing revision and the delivered fixture configuration. A dated inspection report identifying the drawing revision, fixture serial or job reference, measured characteristics, and acceptance status. Check that the report is complete, traceable to the delivered item, and consistent with the latest approved drawing and purchase requirements.

Note: ISO 2768-1:1989 addresses general tolerances for specified dimensions; it does not establish a universal CMM requirement or a universal repeatability threshold. Define project-specific acceptance criteria on the drawing or purchase specification.

How to Compare Leading Chinese Manufacturers Across Five Capability Metrics

Who Are the Top Part Fixture Manufacturers in China?

Compare suppliers through five practical metrics: positioning accuracy, part-size range, inspection controls, engineering response, and delivery reliability. Request drawings, tolerance records, and sample inspection reports. A fixture that repeatedly locates a part within a few hundredths of a millimeter can reduce adjustment time, but only when the measurement method is clear.

Deloitte’s 2024 Smart Manufacturing Survey found that 86% of surveyed manufacturing executives see smart manufacturing as a primary driver of competitiveness within five years. For fixture buyers, this makes digital inspection records and process traceability useful comparison points—not automatic proof of quality. Ask how a supplier handles design changes, replacement components, and unexpected production delays. A polished certificate wall is not enough. I would still verify the details against a real sample.

Tips: Send the same drawing and inspection checklist to each candidate. Compare quoted lead time with recent delivery records, and ask for one example of a corrected fixture issue. A small gap in the paperwork may matter.

Supplier Verification: ISO 9001:2015, IATF 16949:2016, and Delivery Performance

When comparing part fixture manufacturers in China, treat certificates as evidence to verify, not a substitute for checking the actual work. ISO’s ISO Survey 2022 recorded about 1.27 million ISO 9001 certificates worldwide. That scale shows how widely the standard is used; it does not show whether a fixture holds tolerance after repeated clamping. Ask for the current certificate, its scope, and the issuing body. Then review inspection records for a recent fixture, including datum checks, calibration status, and corrective actions. Small details matter.

For automotive programs, verify that IATF 16949:2016 certification covers the manufacturing site and relevant activities. Confirm this against the certificate and current audit status, rather than relying on a supplier’s brochure. Delivery needs its own evidence. Request a 6–12-month record of on-time delivery, agreed dates, actual shipment dates, and corrective actions for late orders. The World Bank’s 2023 Logistics Performance Index ranked China 19th overall and includes timeliness among its measures. That is useful country-level context, not a forecast for one factory. A spreadsheet can still hide partial shipments or revised promise dates. Ask how those are counted. One uncomfortable question: does the reported delivery rate include urgent orders that displaced other customers’ work?