China Best Comprehensive Checking Fixture Supplier?
Choosing the China Best Comprehensive Checking Fixture Supplier requires more than comparing prices. Automotive programs now demand repeatable dimensional control, fast engineering changes, and traceable inspection records. A fixture may look impressive on a factory floor, yet still fail when datum strategy, material stability, or gauge repeatability is overlooked.
The International Federation of Robotics, in World Robotics 2024, reported approximately 135,000 new robots installed by automotive manufacturers worldwide in 2023. Higher automation increases the need for accurate fixtures that verify body panels, welded assemblies, battery trays, and interior components. The International Energy Agency’s Global EV Outlook 2024 also recorded nearly 14 million electric car sales in 2023. This growth creates new inspection challenges, especially for large battery structures and mixed-material assemblies. Therefore, a reliable Comprehensive Checking Fixture supplier should demonstrate experience with CMM data, GD&T interpretation, modular tooling, and production-line validation.
Supplier evaluation should include design reviews, prototype evidence, inspection reports, and response records after tooling changes. IATF 16949 practices and ISO 9001 systems can support consistency, but certificates alone prove little. Practical evidence matters more. Ask to inspect calibration labels, datum pins, clamps, reference points, and the final gauge repeatability study. No fixture is perfect. Even experienced teams can miss accessibility, thermal expansion, or operator ergonomics during early design. That weakness deserves honest review. The strongest Chinese supplier combines engineering depth, controlled manufacturing, clear communication, and measurable quality results. This article examines those criteria and identifies what buyers should verify before selecting a long-term partner.
What Defines a Comprehensive Checking Fixture in China’s Automotive Industry?
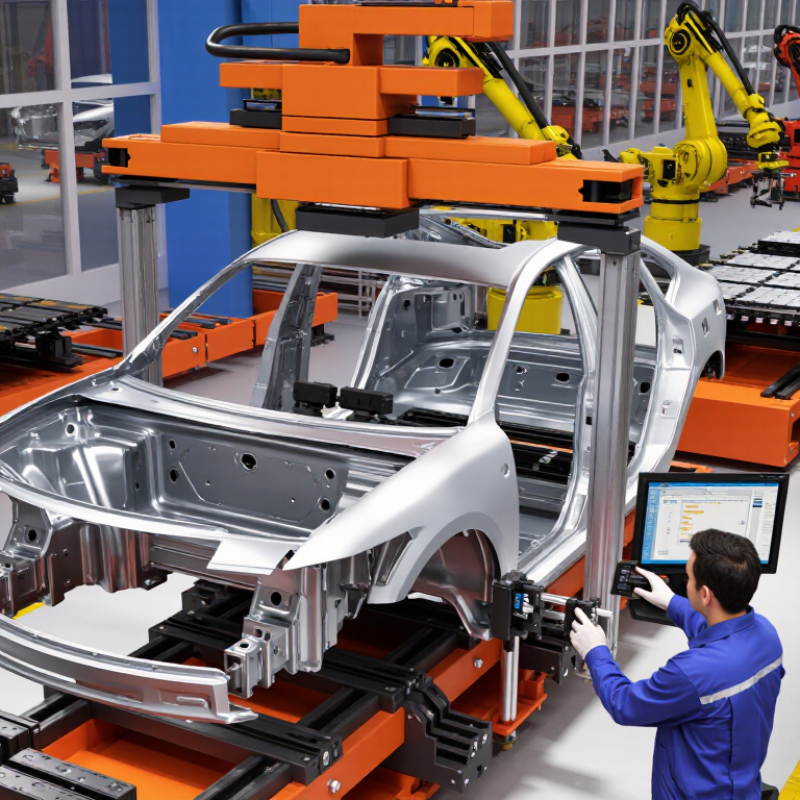
A comprehensive checking fixture is more than a metal frame with locating pins. In China’s automotive industry, it verifies body panels, doors, closures, and assemblies against design intent. It combines datum control, functional gauges, clamping points, and measurement access. On a production line, operators should load a panel quickly and repeatably, without forcing it into position. Small details matter, such as hardened locators, adjustable supports, clear part-number marking, and safe hand clearance.
China produced 31.28 million vehicles in 2024, while sales reached 31.44 million, according to the China Association of Automobile Manufacturers. This scale increases pressure on fixture suppliers to support stable inspection and fast model changes. A capable supplier should interpret GD&T drawings, manage tolerance stack-ups, and verify fixtures with CMM reports. Digital records should connect fixture revisions with inspection results and corrective actions. It should support both conventional steel panels and complex new-energy vehicle structures.
The best supplier is not defined by a polished showroom. It is defined by repeatability under factory conditions. Temperature changes, operator variation, and worn locators can affect results. ISO 9001 quality systems help, but certificates alone are insufficient. The supplier should provide calibration evidence, gauge R&R studies, maintenance instructions, and practical training. According to automotive quality guidance from AIAG, measurement-system variation must remain controlled before process decisions become trustworthy. Some fixtures still look precise but lack clear replacement plans. That is a weakness worth challenging.
Why IATF 16949 and PPAP Compliance Matter in Supplier Selection
China Best Comprehensive Checking Fixture Supplier?
Selecting a comprehensive checking fixture supplier requires more than comparing prices or machining photos. IATF 16949 certification shows that a supplier follows a controlled automotive quality system. It supports traceability, risk management, corrective action, and process consistency.
This matters when a fixture checks several body panels or assembly points. Engineers need stable datum references, repeatable clamps, and clear inspection records. A reliable supplier should control drawings, calibration dates, material certificates, and design revisions. Small changes can affect fit, measurement results, and production timing.
PPAP compliance adds practical evidence. The supplier should provide dimensional results, material records, process documents, control plans, and capability data when required. These documents help customers judge whether the fixture can support an approved production process. Customer-specific requirements must also be reviewed carefully.
Paperwork alone is not enough.
During supplier audits, ask how operators handle a failed measurement. Check whether nonconforming parts are isolated and investigated. Review sample reports instead of accepting general promises. A qualified supplier can explain its inspection method in plain language.
Still, no system is flawless. Delayed feedback, unclear tolerances, or late engineering changes can create avoidable problems. I have seen projects suffer because teams trusted certificates without checking actual measurement practice. Supplier selection should combine IATF 16949 evidence, PPAP discipline, technical experience, and honest communication. Reliability is built through repeated, verifiable actions.
Why IATF 16949 and PPAP Compliance Matter in Supplier Selection
PPAP has five submission levels defined by AIAG. The chart presents their relative documentation scope, from a warrant-only submission to a complete submission package with full supporting records.
A supplier with an IATF 16949 quality management system and demonstrated PPAP capability can provide stronger evidence of process control, traceability, risk management, and production readiness before approval.
How AIAG MSA GR&R Targets Below 10% Verify Measurement Reliability
China Best Comprehensive Checking Fixture Supplier?
A reliable checking fixture must prove more than dimensional accuracy. Its measurement system should produce repeatable, trustworthy results. AIAG MSA GR&R helps evaluate this performance through repeated measurements by different operators. A study below 10% GR&R is generally considered acceptable for many production decisions. The result indicates that fixture variation remains small compared with total process variation. However, the acceptance limit should match product risk and customer requirements.
For practical verification, select representative parts across the expected tolerance range. Use at least two operators and repeat each measurement several times. Record clamping force, datum contact, temperature, and probe condition. These details can expose hidden fixture variation. A fixture may appear stable during one inspection, yet perform differently after cleaning or adjustment. That is easy to overlook. Poor operator instructions can also distort the result.
Tips:
Check the fixture’s zero point before every study. Keep operators from seeing earlier readings. Review the X-bar chart for unusual patterns. If GR&R exceeds 10%, inspect locating pins, supports, gauges, and measurement technique before changing the acceptance rule. In our experience, rushing the study creates false confidence. We also need to admit that one successful report cannot prove long-term reliability. Repeating the study after maintenance or process changes provides stronger evidence.